
Equipment that travels rarely fails because of poor operation. It fails because of poor packaging. Whether it is a construction survey rig heading to a remote site, a touring production’s lighting rack, or an architecture firm’s precision scanning equipment, the difference between arriving ready to work and arriving in for repair usually comes down to one thing: the case it travelled in. This is the discipline of Road Case Designer work – engineering enclosures that are built to absorb impact, resist environmental stress, and keep sensitive equipment stable through repeated handling. For firms that rely on expensive, calibrated, or fragile assets, understanding how this design process works is the first step to protecting a serious investment.
What Is Road Case Design?
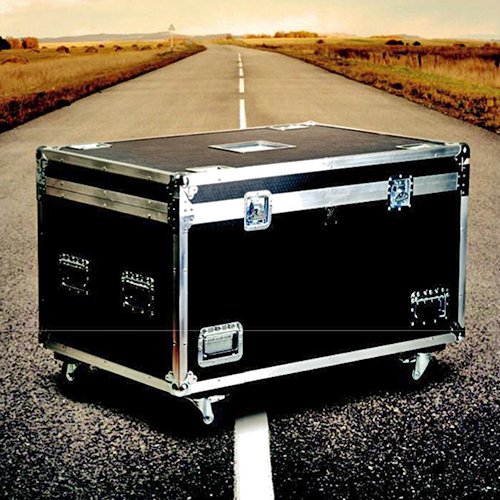
Road case design is the engineering process of building protective transit enclosures – often called flight cases – that shield equipment from shock, vibration, moisture, dust, and mishandling during transport. Unlike generic packaging, a road case is engineered around the exact dimensions, weight, and fragility of the item it carries.
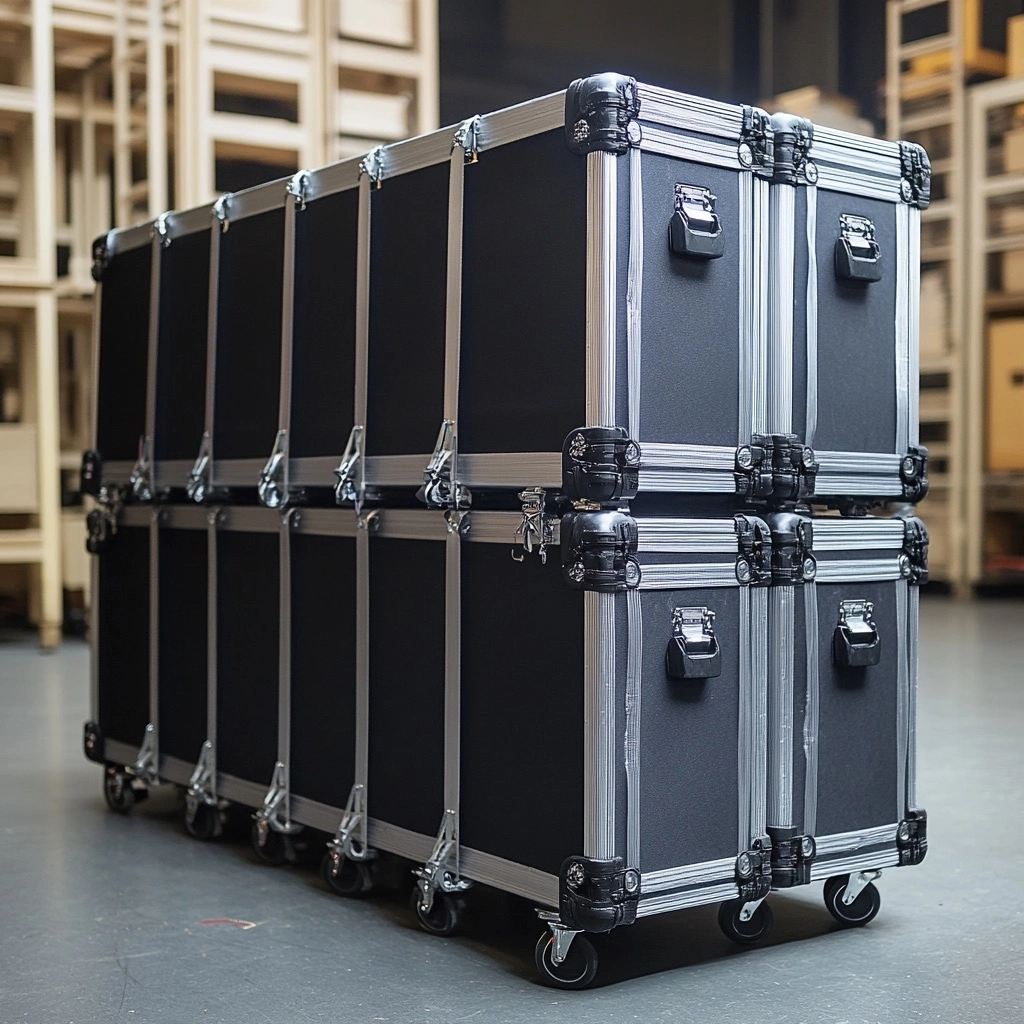
A well-designed case does three jobs at once: it protects the contents, it makes the equipment easier to move and store, and it withstands years of repeated freight handling, stacking, and loading without failing. This combination of protection, usability, and durability is what separates professional road case design from standard shipping boxes.
Why Equipment Protection Matters During Transport and Touring
For engineering, construction, and architecture firms, equipment such as total stations, 3D scanners, drones, and testing instruments is often calibrated to fine tolerances. A single hard knock during freight handling can throw off readings long before anyone notices the fault.
Touring and event production equipment faces a different but equally demanding challenge: repeated loading and unloading, sometimes several times a week, over months. The cumulative wear from this cycle is what most often causes failures, not any single dramatic incident.
Poorly protected equipment leads to project delays, costly recalibration or replacement, and – in hiring and staffing terms – reputational risk for firms whose professionals turn up without functioning tools. Investing in proper transit protection is a practical risk-management decision, not an aesthetic one.
Core Engineering Principles Behind Effective Road Case Design
Professional case builders work to a set of established engineering principles rather than guesswork. These principles determine how a case behaves under real-world transport conditions.
1. Impact Absorption
Foam inserts, corner blocks, and internal cushioning are calculated to absorb and dissipate shock energy before it reaches the equipment, rather than transferring the full force of an impact directly to the contents.
2. Load Distribution
Weight must be spread evenly across the case base and reinforced corners. Uneven load distribution is a common cause of warping, hinge failure, and stress cracks over a case’s working life.
3. Vibration Isolation
Sustained low-level vibration from road or air freight can loosen fasteners and degrade sensitive electronics over time. Isolation mounts and layered foam reduce this transmitted vibration significantly.
4. Environmental Sealing
Gasket seals, weatherproof latches, and moisture-resistant panels protect against humidity, dust, and temperature swings, particularly relevant for outdoor construction sites or international touring.
Together, these principles form the foundation of every credible
Road Case Design project, regardless of whether the case is holding surveying instruments or stage lighting consoles.
Key Materials Used in Road Case Construction
Material choice directly affects a case’s strength-to-weight ratio, cost, and lifespan. Most professional cases combine several materials rather than relying on one.
- Plywood shells: typically 9–12mm birch or poplar ply, offering strength and screw retention for hardware.
- Aluminium extrusion edging: protects corners and edges, the most vulnerable points on any case.
- ABS or polyethylene laminate: a durable, weather-resistant outer skin bonded to the plywood.
- Foam inserts: closed-cell polyethylene or polyurethane foam, cut to the exact profile of the equipment.
- Heavy-duty hardware: recessed butterfly latches, ball corners, and spring-loaded handles rated for repeated use.
The right combination depends on how the case will be used – a case that is loaded onto a truck twice a year has different requirements to one loaded and unloaded at a different venue every night.
How a Road Case Designer Approaches a Custom Build
A qualified road case designer does not start with a template. The process typically follows a structured sequence to ensure the finished case matches both the equipment and the way it will actually be used.
Step 1: Equipment Assessment
The designer records exact dimensions, weight, fragile points, and any ventilation or access requirements for the equipment in question.
Step 2: CAD Modelling
Using AutoCAD or equivalent design software, the internal layout, foam cutouts, and case shell are modelled precisely before any material is cut. This stage is where measurement errors are caught before they become costly.
Step 3: Prototyping and Testing
A prototype is built and, where appropriate, tested against drop, vibration, or load standards relevant to the equipment’s use case.
Step 4: Production and Finishing
The final case is manufactured, fitted with hardware, and finished with branding, labelling, or asset-tracking features as required.
This structured, CAD-led approach is why firms that rely on precision equipment increasingly look for designers with genuine engineering and drafting skill, rather than treating case-building as a simple carpentry task.
Common Risks During Transport and How Design Mitigates Them
Understanding the specific risks equipment faces in transit helps explain why each design choice matters.
- Drops and impacts – mitigated by corner reinforcement, recessed hardware, and internal foam cushioning.
- Compression from stacking – mitigated by rigid shell construction and load-bearing corner blocks.
- Vibration during long-haul freight – mitigated by isolation foam and secure internal mounting.
- Moisture and dust ingress – mitigated by gasket seals and weatherproof latch systems.
- Repeated handling wear – mitigated by heavy-duty hinges, ball corners, and reinforced wheel assemblies.
None of these risks are eliminated entirely – they are managed to an acceptable, calculated level, which is the realistic goal of any transit protection system.
Best Practices for Choosing the Right Road Case
Firms evaluating case options, or hiring designers to build them, should look for a few consistent markers of quality work.
- Custom internal fitting rather than generic foam padding.
- Clear documentation of materials and hardware ratings.
- Evidence of CAD-based design rather than freehand fabrication.
- A track record with equipment of similar weight and fragility to your own.
- Realistic guidance on maintenance and expected working life.
For a deeper walkthrough of the selection process, this guide to choosing a road case designer covers the questions worth asking before committing to a build.
Conclusion: Protecting Equipment Starts With Good Design
Reliable equipment protection during transport and touring is not accidental – it is the result of deliberate engineering decisions made long before a case is ever loaded onto a truck. From material selection to CAD-modelled internal fitting, every stage of the process exists to reduce risk to valuable, often irreplaceable, equipment.
For engineering, construction, architecture, and production teams that depend on their equipment arriving ready to work, Keyway applies exactly this kind of precision engineering approach to every case it designs, drawing on genuine CAD and drafting expertise rather than off-the-shelf templates. Firms exploring custom transit protection, or looking to bring skilled design capability into their own teams, can find further insight and updates via keyway on LinkedIn.